What recent studies examine
A February 2026 study in Machines evaluates EfficientNet-B0 for detecting defective photovoltaic modules using electroluminescence inspection images. Separate 2026 research examines anomaly detection across multiple module-manufacturing lines, where image distributions can differ between equipment and production conditions.
These studies focus on image-based defect detection and diagnosis. They do not establish a universal physical defect-size threshold, production-line accuracy figure or scrap-reduction rate for all factories.
Image resolution is not a defect-size guarantee
A camera's pixel scale, optical resolution, lighting, module position and image-processing pipeline affect what an inspection system can observe. Detection performance also depends on defect type, contrast, sample representation, annotation quality and the threshold chosen for action.
A model score on a research dataset is not the same as a validated physical measurement. To state a minimum detectable crack width or weld displacement, a supplier must define the measurement setup, calibrated reference, uncertainty and production acceptance protocol.
Where machine vision can add value
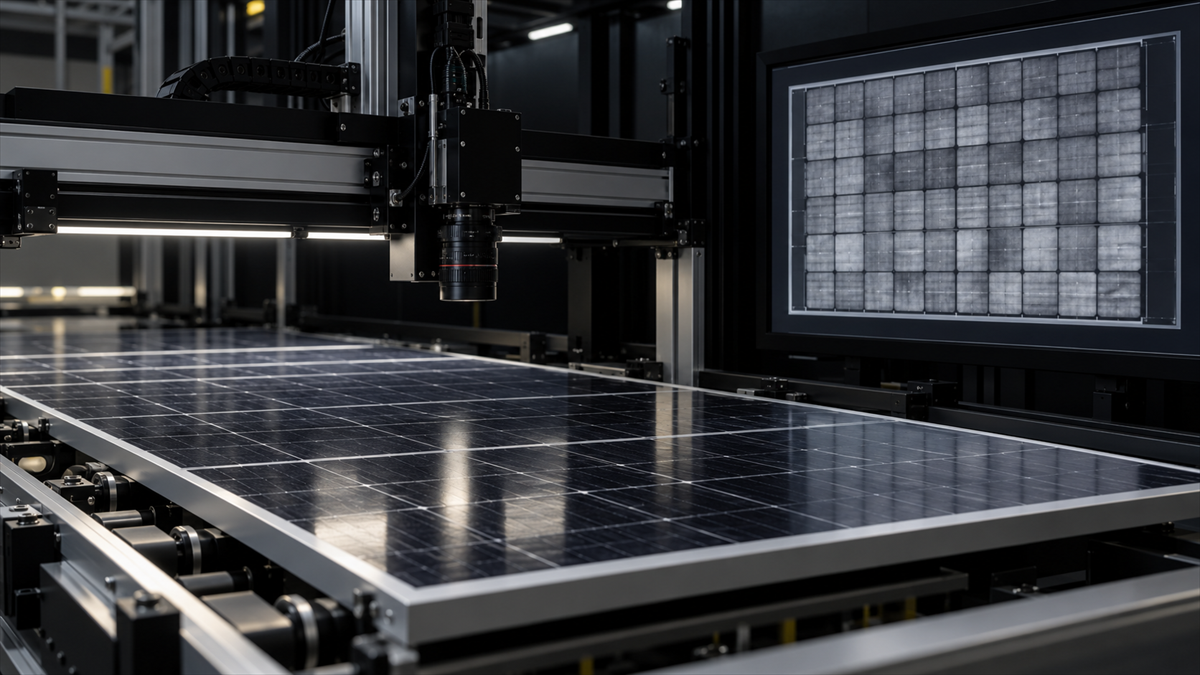
Automated image review can help sort electroluminescence patterns, flag candidate defects and direct human review toward unusual cases. It can improve consistency and throughput when the model is validated against representative production data and integrated into a documented quality process.
Line-to-line variation creates a further challenge: a model trained on one process may not transfer unchanged to another. Monitoring for data drift, maintaining traceability and preserving an escalation path are part of a reliable inspection system.
What a buyer or auditor should request
Request the inspection modality, defect taxonomy, dataset scope, validation design, false-accept and false-reject definitions, threshold-setting method and evidence from the production line that supplied the product.
If a supplier cites a millimetre-scale capability or a percentage improvement, ask for the calibrated measurement report and baseline. Without those details, treat the number as an unverified claim rather than a purchasing specification.
The next evidence step
The most decision-useful research will test models on held-out lines and time periods, report per-defect performance and demonstrate how model flags affect verified quality outcomes. Until then, machine vision is a promising inspection aid—not a substitute for a defined acceptance standard.
Frequently asked questions
What did the February 2026 machine-vision study investigate?
It investigated EfficientNet-B0 for detecting defective photovoltaic modules from electroluminescence inspection images. Its results apply to the study's dataset and validation setup.
Can image resolution alone prove detection of a specific physical defect size?
No. A physical-size detection claim needs a calibrated optical and measurement setup, defined defect sample, uncertainty analysis and validated decision threshold. Pixel count by itself is insufficient.
Does AI inspection replace module quality testing?
No. Image models can support inspection and triage, but product qualification, calibrated measurements, traceability and contractual acceptance checks remain necessary.
Use the news as a project input, then verify the scope.
This News item is editorial context. Confirm the final datasheet, applicable standard, project conditions and acceptance evidence before changing a design or purchase decision.
Discuss a project implication